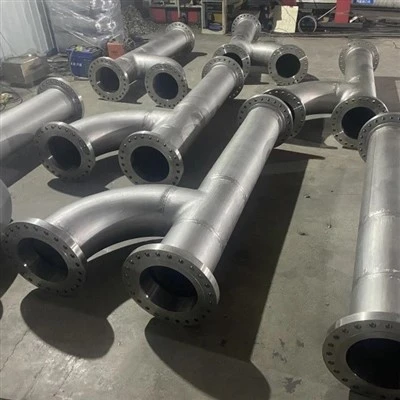
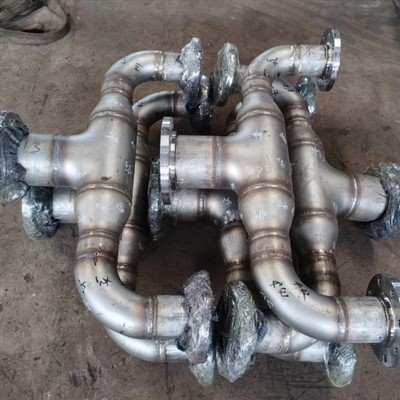
Every weld deposits energy into the base metal. That energy, measured as heat input, directly controls the size of the heat-affected zone (HAZ), the cooling rate, and ultimately the microstructure and properties of the welded joint. For stainless steels, where corrosion resistance is the primary performance requirement, heat input control is not optional -- it is fundamental.
Heat input is calculated from three welding parameters: amperage (current), voltage, and travel speed. The relationship is straightforward: heat input equals the product of current and voltage, divided by travel speed, with a correction factor for the welding process. Yet despite this simplicity, heat input remains one of the most misunderstood and misapplied parameters in stainless steel fabrication.

Why does it matter more than you think? Because the consequences of incorrect heat input are not always visible immediately. A weld that passes visual inspection and radiography may still fail in service due to sensitization, sigma phase formation, or excessive grain growth -- all of which are directly linked to the thermal cycle imposed during welding. This article explains the metallurgical basis for heat input limits and provides practical guidance for different stainless steel families.
Heat Input Calculation
The standard formula for heat input is derived from basic physics. Power (watts) equals voltage multiplied by current. Energy (joules) equals power multiplied by time. In welding, we are interested in energy per unit length of weld, which means we divide by the travel speed.
The efficiency factor accounts for heat lost to the surroundings -- radiation, convection, and spatter. Different welding processes have different efficiencies:
Table 1: Heat Input Efficiency Factors by Welding Process
|
Welding Process |
Efficiency Factor (k) |
Typical Heat Input Range |
|
SMAW (Shielded Metal Arc) |
0.70 - 0.85 |
1.0 - 3.0 kJ/mm |
|
GMAW (Gas Metal Arc) |
0.75 - 0.90 |
0.8 - 2.5 kJ/mm |
|
GTAW (Gas Tungsten Arc) |
0.60 - 0.70 |
0.5 - 2.0 kJ/mm |
|
SAW (Submerged Arc) |
0.90 - 0.99 |
2.0 - 5.0 kJ/mm |
|
FCAW (Flux Cored Arc) |
0.75 - 0.90 |
1.0 - 3.0 kJ/mm |
Source: AWS D1.6:2017; ASME Section IX (2023); Welding Metallurgy, Kou (2003)
Example calculation: A GTAW weld made at 12 volts, 150 amperes, and a travel speed of 150 mm/min: Heat input = (12 x 150 x 0.6 x 60) / (150 x 1000) = 0.43 kJ/mm. This is a relatively low heat input, typical for thin-section austenitic stainless steel.
Austenitic Stainless Steels: Moderate Heat Input Prevents Sensitization
Austenitic stainless steels are the most weldable of all stainless families, but they are not immune to thermal damage. The primary risk is sensitization -- the precipitation of chromium carbides at grain boundaries when the metal passes through the 500-850 degrees Celsius range. High heat input extends the time the HAZ spends in this critical temperature zone, increasing the severity of sensitization.

Low-carbon grades (304L, 316L) and stabilized grades (321, 347) were developed specifically to resist sensitization. However, even these grades are not immune to the effects of excessive heat input. High heat also causes grain growth, which can reduce toughness and increase the risk of hot cracking in fully austenitic weld metals.
The recommended heat input range for austenitic grades balances two competing requirements: enough heat to ensure adequate fusion and weld pool fluidity, but not so much that the HAZ spends excessive time in the sensitization range. Interpass temperature control (typically below 150 degrees Celsius) further reduces the cumulative thermal exposure.
Table 2: Heat Input Guidelines for Austenitic Stainless Steels
|
Grade |
Recommended Heat Input |
Maximum Interpass Temp |
Primary Risk of Excessive Heat |
|
304 / 304L |
1.0 - 2.5 kJ/mm |
150 C |
Sensitization, grain growth |
|
316 / 316L |
1.0 - 2.5 kJ/mm |
150 C |
Sensitization, reduced corrosion resistance |
|
321 (Ti-stabilized) |
1.0 - 2.5 kJ/mm |
200 C |
Grain growth, reduced toughness |
|
347 (Nb-stabilized) |
1.0 - 2.5 kJ/mm |
200 C |
Grain growth, fissuring risk |
|
310 / 310S |
0.8 - 2.0 kJ/mm |
150 C |
Hot cracking, grain growth |
Source: Outokumpu Stainless Steel Handbook (2020); AWS D1.6:2017; ASME Section VIII Div.1 (2023)
Duplex Stainless Steels: Heat Input Controls the Austenite-Ferrite Balance
Duplex stainless steels derive their exceptional strength and corrosion resistance from a balanced microstructure of approximately 50% austenite and 50% ferrite. Welding disrupts this balance. The rapid thermal cycle favors ferrite formation, and if heat input is too low, the weld metal and HAZ can retain excessive ferrite (above 70%), which reduces toughness and corrosion resistance.
Conversely, if heat input is too high, the extended time at elevated temperature promotes the formation of harmful intermetallic phases -- particularly sigma phase and chi phase. These phases consume chromium and molybdenum from the surrounding matrix, creating depleted zones susceptible to pitting and stress corrosion cracking. Sigma phase formation is the most serious metallurgical risk in duplex welding.
The solution is a carefully controlled heat input window, combined with appropriate filler metals. Filler metals for duplex grades are over-alloyed with nickel (typically 8-9%) to promote austenite reformation during cooling. The heat input must be high enough to allow time for this austenite transformation, but not so high that sigma phase forms.
Table 3: Heat Input Guidelines for Duplex Stainless Steels
|
Duplex Grade |
Heat Input Range |
Max Interpass |
Cooling Rate Requirement |
Target Phase Balance |
|
2205 (UNS S31803) |
0.5 - 2.5 kJ/mm |
150 C |
Not critical if within range |
45-55% austenite |
|
2507 (UNS S32750) |
0.5 - 2.0 kJ/mm |
150 C |
Moderate cooling preferred |
45-55% austenite |
|
2304 (UNS S32304) |
0.5 - 2.5 kJ/mm |
150 C |
Not critical |
45-55% austenite |
|
Lean Duplex (2101) |
0.8 - 2.5 kJ/mm |
150 C |
Faster cooling acceptable |
40-60% austenite |
Source: Outokumpu Duplex Stainless Steel Handbook (2015); Sandvik SAF 2205/2507 Welding Guidelines; NACE MR0175/ISO 15156
Martensitic Stainless Steels: Low Heat Input with Preheat Prevents Cracking
Martensitic stainless steels transform to hard, brittle martensite upon cooling from the austenitizing temperature. This transformation creates high residual stresses and makes the HAZ extremely susceptible to hydrogen-induced cracking (also called delayed cracking or cold cracking). Unlike austenitic grades, martensitic steels are not protected by a stable FCC crystal structure.
Heat input control for martensitic grades serves two purposes. First, excessive heat input increases the size of the hardened HAZ, creating a larger volume of brittle material. Second, low heat input combined with preheating slows the cooling rate, which reduces the hardness of the martensite and provides more time for hydrogen to diffuse out of the weld zone.

Preheating is essential for martensitic grades. The preheat temperature depends on the carbon content and section thickness, but typically ranges from 200-300 degrees Celsius. Interpass temperature must be maintained above the preheat minimum. Post-weld heat treatment (tempering at 650-750 C) is almost always required.
Table 4: Heat Input and Preheat Requirements for Martensitic Stainless Steels
|
Martensitic Grade |
Carbon Content |
Recommended Heat Input |
Preheat Temp |
PWHT Required |
|
410 (UNS S41000) |
0.08-0.15% |
1.0 - 2.0 kJ/mm |
200-300 C |
Yes (temper) |
|
420 (UNS S42000) |
0.16-0.25% |
0.8 - 1.5 kJ/mm |
250-350 C |
Yes (temper) |
|
431 (UNS S43100) |
0.12-0.22% |
0.8 - 1.5 kJ/mm |
200-300 C |
Yes (temper) |
|
17-4PH (UNS S17400) |
0.07% max |
1.0 - 2.0 kJ/mm |
100-150 C |
Yes (aging) |
Source: ASM Specialty Handbook: Stainless Steels (1994); AWS D1.6:2017; ASME Section VIII Div.1
Cooling Rate Connection: Why Heat Input Alone Is Not Enough
Heat input is a measure of energy deposited, but it is the cooling rate that determines the final microstructure. The same heat input applied to a 3 mm sheet will produce a much faster cooling rate than when applied to a 25 mm plate. This is why heat input recommendations must always be considered alongside section thickness.
The cooling rate in welding is typically measured as the time to cool from 800 to 500 degrees Celsius (t8/5). For carbon steels, this parameter directly determines the hardness and microstructure of the HAZ. For stainless steels, the critical temperature range differs -- for sensitization, it is the time spent between 850 and 500 degrees Celsius that matters.
The relationship between heat input and cooling rate can be approximated using heat flow equations. For thin sections (where heat flows primarily in two dimensions), cooling rate is inversely proportional to the square of heat input. For thick sections (three-dimensional heat flow), cooling rate is inversely proportional to heat input. This means that in thin sections, a small increase in heat input dramatically slows the cooling rate.
Table 5: Cooling Rate Variation with Heat Input and Section Thickness
|
Section Thickness |
Heat Input 1.0 kJ/mm |
Heat Input 2.0 kJ/mm |
Heat Input 3.0 kJ/mm |
Effect on HAZ |
|
3 mm (thin) |
Very fast cooling |
Fast cooling |
Moderate cooling |
Minimal sensitization risk |
|
10 mm (medium) |
Fast cooling |
Moderate cooling |
Slow cooling |
Sensitization risk increases |
|
25 mm (thick) |
Moderate cooling |
Slow cooling |
Very slow cooling |
High sensitization risk |
Source: Welding Metallurgy, Kou (2003); ASM Handbook Volume 6A (2011)
Multi-Pass Welding: Cumulative Heat Input and Interpass Temperature
Multi-pass welding introduces a complication that single-pass welding does not have: each subsequent pass subjects the underlying weld metal and HAZ to additional thermal cycles. This can be beneficial or harmful depending on the grade. For some austenitic welds, the heat from later passes can dissolve carbides formed during earlier passes. For duplex grades, repeated heating into the 600-900 degrees Celsius range accelerates sigma phase formation.
Interpass temperature is the temperature of the weld zone just before depositing the next pass. For most stainless steels, this should be kept below 150 degrees Celsius to limit cumulative thermal exposure. Some duplex specifications are even more restrictive, requiring interpass below 100 degrees Celsius for super-duplex grades like 2507.
The practical implication is that multi-pass welds require more careful planning than single-pass welds. The welder must allow sufficient time between passes for cooling, or use forced cooling methods (air blast, water mist) that do not contaminate the weld zone. Rushing multi-pass welding on duplex or super-duplex grades is a common cause of sigma phase formation and subsequent service failures.
Table 6: Interpass Temperature Guidelines for Multi-Pass Welding
|
Grade Family |
Recommended Interpass |
Maximum Passes Without Cooling |
Critical Monitoring Point |
|
Austenitic (304, 316) |
150 C max |
3-4 typical |
Time in sensitization range |
|
Duplex (2205) |
150 C max |
2-3 typical |
Sigma phase formation |
|
Super-Duplex (2507) |
100 C max |
2 recommended |
Sigma phase, intermetallics |
|
Martensitic (410, 420) |
Maintain above preheat |
No limit if preheated |
Hydrogen cracking |
|
Nickel Alloys (625, C-276) |
150 C max |
3-4 typical |
Grain growth, microsegregation |
Source: Outokumpu Welding Guidelines (2020); Special Metals Welding Handbook; NACE MR0175
Consequences of Excessive Heat Input
The consequences of poor heat input control are not theoretical. They appear regularly in failure analysis reports across industries. Understanding these failure modes helps engineers and inspectors recognize the symptoms and trace them back to the root cause.
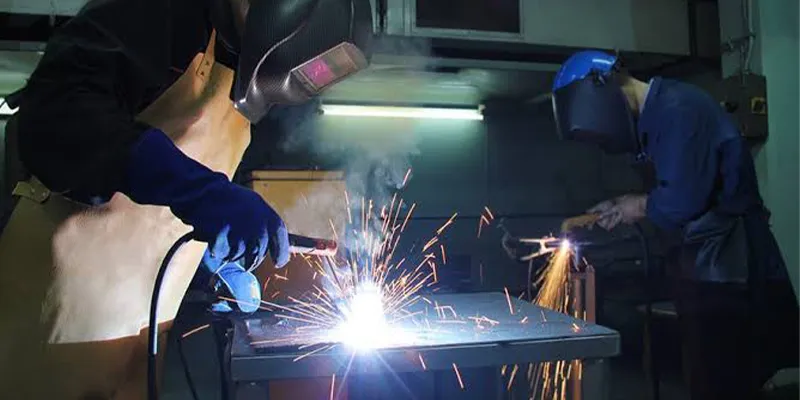
Intergranular corrosion: Caused by sensitization in the HAZ. The grain boundaries are selectively attacked, leading to a 'sugaring' appearance on the surface. Common in 304/316 welds with excessive heat input without proper L-grade or stabilization.
Pitting corrosion: Sigma phase formation in duplex steels consumes chromium and molybdenum, creating zones with reduced pitting resistance. Pits initiate preferentially in the HAZ of high-heat-input welds.
Stress corrosion cracking (SCC): High heat input creates larger HAZ with higher residual stress. Combined with sensitization, this creates ideal conditions for SCC in chloride-containing environments.
Reduced toughness: Excessive grain growth in austenitic HAZ reduces impact toughness. In duplex steels, high ferrite content and sigma phase both reduce toughness significantly.
Hot cracking: In fully austenitic weld metals (310, some nickel alloys), high heat input extends the time spent in the brittle solidification range, increasing the risk of solidification cracking.
Table 7: Failure Modes Linked to Excessive Heat Input
|
Failure Mode |
Primary Cause |
Grades Most Affected |
Prevention |
|
Intergranular corrosion |
Sensitization in HAZ |
304, 316 (non-L grades) |
Use L-grade, limit heat input |
|
Pitting in HAZ |
Sigma phase, Cr/Mo depletion |
2205, 2507 duplex |
Limit heat input, control interpass |
|
Stress corrosion cracking |
Sensitization + residual stress |
All austenitic grades |
Solution anneal, reduce stress |
|
Reduced impact toughness |
Grain growth, sigma phase |
304, 316, 2205 |
Limit heat input, use proper filler |
|
Hot cracking |
Extended solidification range |
310, 347, some Ni alloys |
Low heat input, proper filler |
Source: ASM Handbook Volume 11: Failure Analysis (2002); NACE Corrosion Data Survey; JN Alloys Failure Case Studies
Practical Heat Input Control: From WPS to Shop Floor
Heat input control begins in the engineering office and ends on the shop floor. The welding procedure specification (WPS) must include explicit heat input limits, not just the basic parameters of amperage, voltage, and travel speed. For critical applications, the WPS should specify the acceptable range for each parameter and the calculated heat input limits.

Specify heat input in the WPS: Do not assume that listing amperage and voltage ranges is sufficient. Calculate and state the maximum heat input explicitly (e.g., 'Maximum heat input: 2.0 kJ/mm').
Use calibrated equipment: Modern power sources can display and record actual amperage and voltage. Use this data to calculate actual heat input, not just the set points.
Train welders on the consequences: Welders who understand that excessive heat input can cause corrosion failures will be more motivated to control travel speed and interpass temperature.
Monitor travel speed: Travel speed is the parameter most often adjusted by welders during production. Provide guidance on how to maintain consistent speed, or use mechanized/automated systems for critical welds.
Document heat input for critical welds: For pressure vessels, offshore components, and chemical plant piping, calculate and record actual heat input for each weld. This provides traceability in case of future failures.
Use heat input calculators: Free apps and online calculators allow welders to quickly compute heat input from the basic parameters. Encourage their use on the shop floor.
The cost of heat input control is minimal compared to the cost of a corrosion failure in service. A single pitting failure in a chemical plant can result in millions of dollars in lost production, environmental cleanup, and equipment replacement. Investing in proper heat input control is not just good engineering -- it is good economics.
Summary
The following table consolidates the recommendations from this article into a quick-reference format. Engineers and fabricators can use this matrix to establish heat input limits for their specific applications.
Table 8: Heat Input Decision Matrix by Stainless Steel Family
|
Stainless Family |
Heat Input Range |
Interpass Max |
Critical Risk |
Key Control Point |
|
Austenitic (304L, 316L) |
1.0 - 2.5 kJ/mm |
150 C |
Sensitization |
Use L-grade, limit time in 500-850 C |
|
Stabilized (321, 347) |
1.0 - 2.5 kJ/mm |
200 C |
Grain growth |
Avoid excessive passes |
|
Duplex (2205) |
0.5 - 2.5 kJ/mm |
150 C |
Sigma phase |
Balance austenite/ferrite |
|
Super-Duplex (2507) |
0.5 - 2.0 kJ/mm |
100 C |
Sigma phase |
Strict interpass control |
|
Martensitic (410, 420) |
0.8 - 2.0 kJ/mm |
Maintain preheat |
Hydrogen cracking |
Preheat + PWHT required |
|
Precipitation-Hardening |
1.0 - 2.0 kJ/mm |
150 C |
Cracking, overaging |
Follow manufacturer spec |
|
Nickel Alloys (625, C-276) |
0.8 - 2.0 kJ/mm |
150 C |
Microsegregation |
Low heat, proper filler |
Source: Compiled from AWS D1.6, ASME Section VIII/IX, Outokumpu, Sandvik, Special Metals, and JN Alloys technical guidelines
Conclusion
Heat input is the single most controllable variable that determines the quality and service performance of stainless steel welds. The metallurgical consequences of heat input -- sensitization, sigma phase formation, grain growth, and phase imbalance -- are well understood and predictable. What is often lacking is the discipline to translate this knowledge into practice.
The recommendations in this article are based on decades of research and field experience. They are not arbitrary limits -- they reflect the underlying physics and metallurgy of welding. By controlling heat input within the appropriate range for each stainless steel family, fabricators can produce welds that retain the corrosion resistance, mechanical properties, and long-term reliability that their customers expect.
For technical support on stainless steel welding procedures, filler metal selection, or heat input optimization, contact JN Alloys -- your partner in high-performance alloy solutions.
Website: www.jnalloys.com